
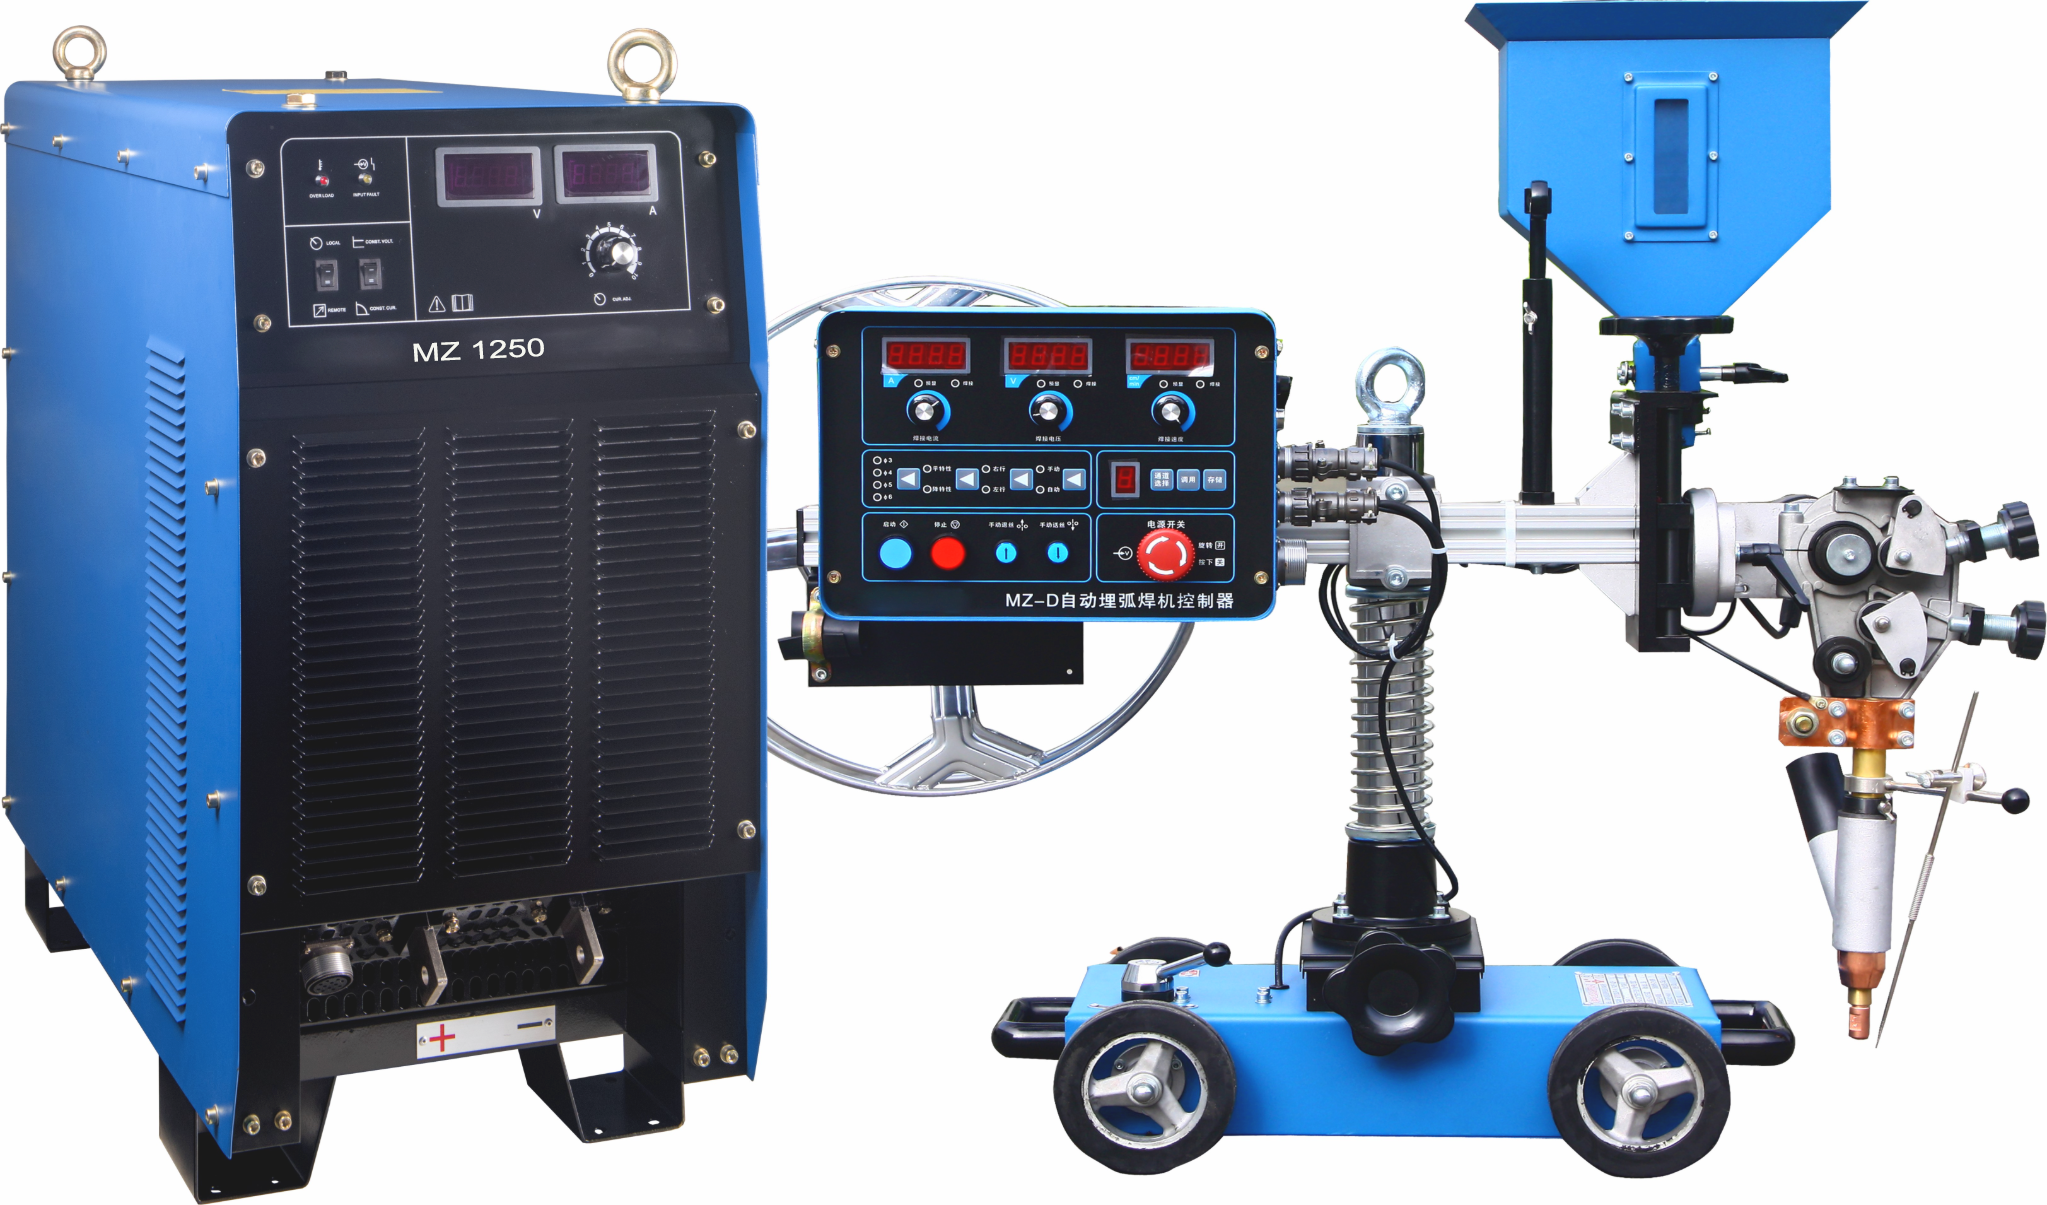
MZ-1250
MZ-1250 is a high-output submerged arc welding power source for heavier mechanized SAW production where weld build-up, deeper penetration demand, and stronger current reserve all increase. It combines 1250A rated output, 100% duty cycle, five-level depth adjustment, and the standard MZ-1 wire feeder package for larger industrial welding tasks.
This model sits between the standard-production and ultra-high-current ends of the MZ lineup, giving buyers a stronger output step for heavier deposition work without moving all the way into the physically larger 1600A and 2000A platforms.
MZ-1250 Technical Specifications
Exact model data for the MZ-1250 power source together with the standard MZ-1 submerged arc wire feeder package used with this machine series.
Power Source
Standard Wire Feeder: MZ-1
High-deposition submerged arc welding for heavier production seam work.
MZ-1250 is positioned for manufacturers who need a meaningful step above 1000A-class SAW power sources, especially when weld volume, joint size, and line throughput all continue to rise.
Made for repetitive mechanized SAW on heavier seams
Submerged arc welding is commonly chosen where the job involves long seam length, repetitive mechanized travel, and thicker joint sections. MZ-1250 is designed to sit comfortably in that heavier-duty production space.
1250A class output for stronger deposition demand
This model expands current reserve beyond standard production SAW power sources, giving fabricators a better fit for larger weld cross-sections and higher-throughput industrial welding schedules.
100% load duration for sustained welding shifts
The published rated-load duration supports the kind of continuous production use normally associated with mechanized submerged arc welding in fabrication plants, vessel shops, and structural lines.
Five-level depth adjustment supports weld-profile tuning
The listed depth adjustment series helps operators refine penetration and weld build-up according to joint design, thickness level, and production target, which is particularly useful as output class increases.
Mechanized feeder package for industrial SAW setup
The included MZ-1 wire feeder supports the wire range, travel adjustment, and positioning movement needed for practical submerged arc welding carriage or seam-travel arrangements in production environments.
Where MZ-1250 fits best
- Heavy plate fabrication and structural welding
- Tank, vessel, and large fabricated shell production
- Industrial SAW lines needing more deposition than 1000A-class systems
Why buyers choose this process
Because the flux blanket shields the arc and weld pool, submerged arc welding remains a strong choice for long seam consistency, deeper fusion potential, and higher productivity on repetitive industrial joints.
Main values buyers compare first
Key values include 1250A rated output current, 66 KVA rated input capacity, 100~1250A current adjustment range, 100% duration of rated load, 88% efficiency, and 85 kg net power weight.
Choose the right MZ submerged arc power source by output level, plant-scale demand, and mechanized welding workload.
The MZ submerged arc lineup scales from compact full-duty production units up to very high-current industrial power sources for heavier deposition demand. All models in this group are paired with the MZ-1 wire feeder platform.
MZ-630 and MZ-1000
- Good fit for general submerged arc production where full-duty performance and manageable machine size matter.
- MZ-630 is the more compact option, while MZ-1000 adds a higher output tier for thicker or faster-running work.
- Suitable for many beam, vessel, and plate-fabrication lines.
MZ-1250
- Steps the series upward for stronger deposition demand and larger weld sections.
- Better suited where the work begins to exceed the comfortable output window of standard production units.
- Acts as the bridge between mid-range and ultra-high-current MZ models.
MZ-1600 and MZ-2000
- Built for very heavy industrial submerged arc applications with larger current reserve and larger machine format.
- Better matched to high-deposition welding, thicker joints, and bigger production lines.
- Best where maximum output matters more than compact equipment size.
Verify the final welding process setup, package scope, and application suitability before ordering.
Published specifications, standard delivery scope, and accessory ratings are for reference only and may change without notice. Power source, wire feeder, welding carriage, torch, flux hopper, control cables, work leads, and other accessories may vary by model, package, and destination market. Before ordering, confirm the required submerged arc welding application, input power, wire diameter, duty cycle, travel arrangement, workpiece material and thickness, and applicable local compliance requirements for the intended installation.